
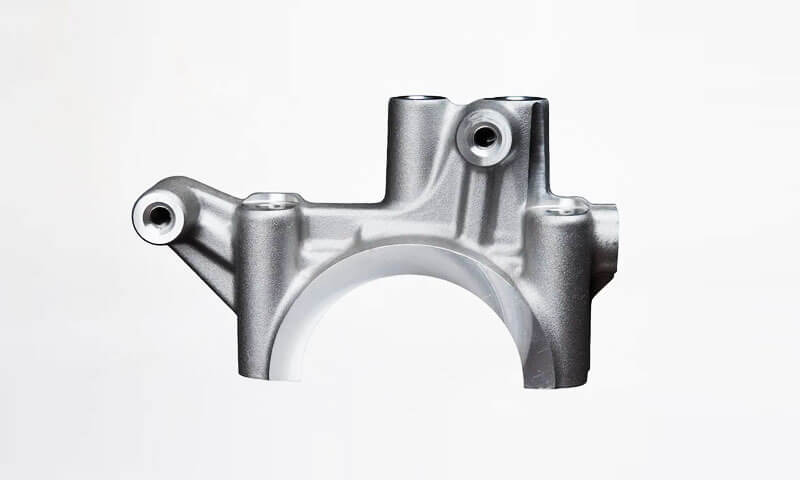
I have been standing next to forging presses for more than thirty years.
I have watched 2xxx aluminum come out of the furnace glowing orange, go under the hammer, and come out either as a beautiful near-net part or as a cracked, folded piece of scrap that goes straight back to the remelt bin.
The difference between those two outcomes is never luck. It is understanding what 2xxx aluminum wants, how it behaves under the hammer, and where its limits are.
In hoc articulum, I will walk you through the forging performance of 2xxx series aluminum alloys from a practical, shop-floor perspective.
We will cover what 2xxx is, why it behaves the way it does, its mechanical and physical profile, forgeability, process windows, calor, corrosion concerns, typical applications, and the mistakes I have seen even experienced shops make.
1. What Are 2xxx Series Aluminum Alloys?
The 2xxx series is the aluminum-copper family. Aeris est prima tinguere elementum, typically sisterent at 3.5% ut 5%.
Small additions of magnesium, manganese, ferrum, Silicon, and sometimes zirconium or titanium refine the structure and improve properties.
Because copper dramatically increases strength, this family earned the name “hard aluminum” or “duralumin” in older literature.
Like 6xxx and 7xxx, 2xxx alloys are æstus-treatable. Solution treatment followed by natural or artificial aging can push strength to very high levels.
The most common grades you will encounter in forging shops are:
| Mixtura | General Characteristics | Typical Forging / Engineering Applications |
| 2A12 | Medium-to-high strength, bona machinability, widely used in China | Structural partes, aerospace-related components, precision forgings |
| 2014 | Excelsum, bona machinability, useful elevated-temperature performance | Aircraft and automotive structural components, high-strength forgings |
| 2024 | Princeps viribus ad-pondus ratio, widely established engineering alloy | Aerospace structurae, caerimonias, aircraft components |
| 2017 | Bona vis et machinabilitas | Fasteners, structural and machined components |
One important engineering point is that 2A12, 2024, et 2014 should not be treated as interchangeable materials, even though they belong to the same alloy family.
Their chemical compositions, Mechanica proprietatibus, heat-treatment conditions, and applicable standards differ.
The correct specification should therefore identify the exigere offensionibus, uber forma, ingenium, and governing material standard.
2. Performance Profile of 2xxx Series Aluminum Alloys
2xxx alloys have a very clear performance profile. Their main advantages are strength, Fortes-ut-pondus Ratio, Machinabilitas, and useful performance in some elevated-temperature applications.
Their main limitations are generally corrosion resistance and fusion weldability.
Excelsum
High strength is usually the first reason an engineer considers a 2xxx alloy.
Depending on the specific grade, ingenium, and product form, 2xxx alloys can provide tensile strengths in the 400–500+ MPa range, while some stronger tempers and alloys can reach substantially higher values.
Pro exemplo, a typical 2A12-T4 product may have tensile strength in approximately the 400–450 MPa range
These figures are useful for engineering comparison, but they should not be treated as universal values.
Minimum guaranteed mechanical properties must always be taken from the applicable material specification.
The important point is that 2xxx alloys occupy a useful position between general-purpose structural aluminum and the highest-strength 7xxx grades.
Good Strength-to-Weight Ratio
A forged 2xxx component can provide high structural performance without the density penalty of steel.
This makes the alloy family attractive when engineers are balancing:
Fortitudo + Pondus + Section Size + Machinabilitas
Typical applications include aerospace fittings, high-strength brackets, structural connections, and other components where reducing mass is important.
The forging process adds another advantage by allowing material to be concentrated around the main load paths instead of starting with a solid block and machining away most of it.
Useful Elevated-Temperature Performance
Some 2xxx alloys have better strength retention at moderately elevated temperatures than many general-purpose 6xxx alloys.
This is one reason certain 2xxx grades have been used in aircraft and engine-related applications.
Tamen, an experienced engineer should be careful with the phrase “high-temperature aluminum”.
2xxx alloys are still aluminum alloys, and their strength decreases as temperature increases.
Actual service-temperature capability depends on the specific grade, ingenium, stress level, tempus expositionis, and required mechanical properties.
For a real component, the correct design question is:
What properties does this alloy and temper retain at the actual operating temperature?
Bonum machinability
2xxx is relatively hard and somewhat brittle. Chips break cleanly. Tool wear is low. Surface finish is good.
If you have ever machined 5056 or a gummy 5xxx alloy, you know what “sticky aluminum” feels like—2xxx is the opposite.
This is precisely why 2xxx is chosen for parts that require extensive CNC finishing after forging.
3. The Main Limitations: Corrosion and Welding
Moderate-to-Poor Corrosion Resistance
Copper and aluminum sit at different electrochemical potentials.
High-copper aluminum is prone to intergranular corrosion and pitting in humid, salt-laden, aut marine environments. 2xxx is clearly inferior to 5xxx and 6xxx in atmospheric corrosion resistance.
For outdoor, maritima, or wet service, 2xxx must be protected—anodizing, cladding, pingitatio, or coating—and galvanic isolation is needed where it contacts steel, aes, aut immaculatam ferro.
Limited Weldability
2xxx is not a welding-friendly family. Conventional fusion welding tends to produce cracking and reduced weld strength.
For welded structures, 5xxx or 6xxx is generally preferred. 2xxx parts are usually joined by mechanical fastening, riveting, et tenaces ad!.
4. Can 2xxx Aluminum Be Forged?
Sic, 2xxx series aluminum alloys can be forged, and many of them are well-established forging materials.
But after years around aluminium cudebat pressis, I would give one simple warning: do not treat 2xxx like 6061 aluminium.
2xxx alloys generally have higher deformation resistance and are more sensitive to forging temperature and deformation conditions.
The process window is therefore less forgiving.
If the billet is too cold, the material becomes difficult to move and cracking or incomplete filling becomes more likely. If it is overheated or held too long, microstructural damage can occur.
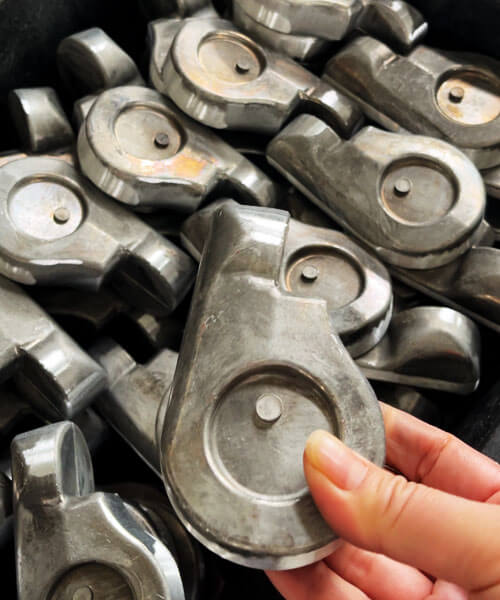
Hot Forging Is the Main Route
For most 2xxx forging applications, controlled hot forging is the practical manufacturing route.
As a broad process reference, initial forging temperatures for alloys such as 2014, 2A12, et 2024 are often in the approximate 430–460°C range,
with the actual working range determined by the specific alloy, billet size, iactabantur rate, mori consilio, and forging equipment.
The minimum finishing temperature must also be controlled; allowing the billet to cool excessively during the final deformation can sharply increase the required forming load.
I would never treat these numbers as a universal recipe. The correct forging window must come from the alloy specification and be validated on the actual production process.
The important thing is temperature uniformity. If the outside of a billet is at the correct temperature while the center is still significantly colder, the press is effectively forging two different materials at the same time.
Ex altera parte, excessive soaking at high temperature can promote grain coarsening or other undesirable metallurgical changes.
quam ob rem calefactio rate, macerari tempore, billet temperature, transfer time, and die temperature all need to be controlled together.
Press Capacity Must Match the Material and Geometry
2xxx alloys generally require higher forming loads than many common 6xxx alloys. But from a forging engineer’s perspective, press tonnage alone is not the answer.
The actual requirement depends on:
Mixtura + Billet Size + Reduction + Pars Geometriae + Die Design + Deformation Sequence
An undersized press can produce incomplete filling, nimia mico, unstable dimensions, and high die loading.
Simply moving the job to a larger press, tamen, will not solve a poor preform or an inefficient material-flow path.
For difficult 2xxx forgings, I normally look at the material distribution before looking for more force.
A well-designed preform can reduce unnecessary local deformation and make much better use of the available press capacity.
Complex Parts May Benefit from Multi-Stage Forming
For relatively simple geometries, a conventional hot-forging sequence may be sufficient. For more complex parts, a pre-forging plus finish-forging route is often more stable.
The first operation distributes the material and establishes the general shape. The finishing operation then completes the critical geometry.
For selected components, a hot-forming operation followed by cold sizing or cold finishing can also improve dimensional accuracy and surface condition.
But this is not automatically the best route for every part. The final process depends on alloy, GEOMETRY, required tolerance, productio volumen, and available equipment.
The old shop-floor rule still applies:
Do not ask the final die to perform all the deformation. Give the material somewhere sensible to flow first.
Material Quality Cannot Be Ignored
2xxx alloys are sensitive to chemistry and metallurgical condition, so starting material quality is critical.
Excessive or uncontrolled impurity levels can affect forgeability, fortitudo, ROSIO, et constantia.
I would not say that every forging-grade 2xxx component must be made exclusively from “primary aluminum”.
The more important requirement is that the billet or wrought stock fully complies with the specified alloy and applicable material standard, with controlled chemistry and traceability.
A good supplier should be able to provide material identification and chemical-composition records rather than simply stating the alloy name on the purchase order.
How DEZE Technology Controls 2xxx Forging
In Xuchang DEZE Technology, 2xxx-series materials such as 2A12 and 2014 are used for applicable precision forging projects.
DEZE operates forging equipment in the 300–2,500 tonne range, together with cold-forging capability, allowing the process to be selected according to component geometry and tolerance requirements.
The manufacturing route can include caligo, cold sizing/forging, or a combined hot-and-cold process where technically appropriate.
Material composition can be verified by spectrometric analysis, with applicable shipments supplied with material and hardness documentation for production traceability.
5. Typical Applications of 2xxx Forged Components
When I look at a 2xxx aluminum forging, I do not start by asking, “Where can this alloy be used?" I start with the load, temperamentum, corrosio environment, ac machining opus.
The reason is simple: 2xxx alloys are chosen primarily for their high strength-to-weight ratio and heat-treatable performance.
Where those properties matter, forging can make particularly good use of the alloy.
The following applications are among the most common for 2xxx forged components.
Aerospace Structural Components
2xxx forged components are widely considered for aerospace and aircraft structural applications where high strength-to-weight ratio and heat-treatable performance are important.
Typical exempla includit:
- Aircraft brackets and fittings
- Structural lugs and clevises
- Adscendens components
- Connection fittings
- High-strength support parts
High-Strength Automotive and Motorsport Parts
2xxx forgings can be considered for selected eget, racing, and performance-oriented components where weight and structural strength are more important than maximum corrosion resistance.
Typical exempla includit:
- High-strength brackets
- Suspension-related components
- Mounting supports
- Steering and chassis fittings
- Specialized structural connectors
Engine and Elevated-Temperature Components
Selected 2xxx alloys can be used for engine-related and moderately elevated-temperature components where useful strength retention and low weight are required.
Typical exempla includit:
- Engine support components
- High-temperature brackets
- Heat-zone structural fittings
- Specialized machinery components
- Lightweight support hardware
Precision Machined Structural Components
2xxx forgings are well suited to components that require substantial CNC machining after forging.
The forging provides the near-net structural shape, while machining creates the precision features required for assembly and function.
Typical exempla includit:
- Housing
- Subtilitas adscendens brackets
- Machined structural fittings
- Components with complex pockets
- Parts with precision bores and threaded holes
Rivets and Structural Fasteners
Some 2xxx alloys are widely associated with high-strength rivets and fastening components, where low weight and mechanical strength are important.
Typical exempla includit:
- Aerospace rivets
- Structural fasteners
- High-strength pins
- Connection hardware
- Specialized fastening components
Jigs, Fixtures, and Tooling Components
Compositum relatively high strength and good machinability makes selected 2xxx alloys suitable for certain engineering tooling and fixture applications.
Typical exempla includit:
- Machining adfixa
- Precision jigs
- Tooling laminis
- Positioning components
- Lightweight support fixtures
6. 2xxx Forging vs. 6xxx and 7xxx: Quam eligere?
| Elementum | 2xxx Series | 6xxx Series | 7xxx Series |
| Main Alloying System | Al-c | Al-mg, si | Al-Zn-Mg, often with Cu |
| Strength Potential | Altum | Ad altum moderari | PERPREPIDUS |
| Forgeability | Bonum, but temperature-sensitive | Generally good and comparatively forgiving | Good for selected grades, but more process-sensitive |
| Forging Temperature Control | Critical; relatively narrow process window | Moderor | Critical; sensitive to temperature and deformation |
| Machinabilitas | Plerumque bonum | Bonum | Plerumque bonum |
| Corrosio resistentia | Moderate to relatively low | Plerumque bonum | Moderor; strongly grade-dependent |
| Weldility | Generally poor for fusion welding | Generally good for common grades | Generally poor for fusion welding |
| Heat-Treatment Response | Praeclarus | Praeclarus | Praeclarus |
| Typical Strength Level | Often around 400–500+ MPa depending on grade and temper | Common structural grades generally lower than 2xxx/7xxx | Excedere potest 500 MPa in high-strength tempers |
| Pondus De reductione Potentia | Altum | Bonum | PERPREPIDUS |
Typical Forging Applications |
High-strength fittings, aerospace components, structural partes, precision forgings | PARTIS, machinamentum, tabulae, general structural components | Aerospace, high-performance structural parts, highly loaded components |
| Best Suited When | Fortitudo, Machinabilitas, and selected elevated-temperature performance are priorities | Balanced strength, corrosio resistentia, and manufacturability are required | Maximum strength-to-weight ratio is the dominant requirement |
| Principalis Limitatio | Lower corrosion resistance and more demanding forging/welding conditions | Lower maximum strength than many 2xxx/7xxx grades | Higher cost and more demanding corrosion/process control |
7. Five Rules I Give Every Young Forging Engineer
After enough years around aluminum forging presses, I have learned that most 2xxx forging problems do not come from one dramatic mistake.
They usually come from ignoring a basic rule. These are the five rules I keep repeating to young forging engineers.
Respect the Corrosion Environment
2xxx alloys are selected primarily for strength, not for maximum corrosion resistance.
In long-term profero, maritima, or salt-spray environments, the material needs an appropriate protection strategy.
Anodizing, pingitatio, cladding, or other protective systems may be required depending on the alloy and application.
When the forged part is assembled with steel, immaculatam ferro, aes, or other dissimilar metals, galvanicum corrosio also needs to be considered.
Do not wait for corrosion to become a field problem. Check the environment when selecting the alloy.
If Welding Is a Major Requirement, Reconsider the Alloy
Many 2xxx alloys are more difficult to fusion weld than common 5xxx and 6xxx alloys.
Welding can introduce cracking, heat-affected-zone softening, and loss of the original heat-treated properties.
For a structure that depends heavily on welding, I would normally investigate a more weldable alloy family first.
Where 2xxx must be used, mechanica ligandi, bolting, or riveting may be more appropriate depending on the design.
The lesson is simple: choose the alloy for the whole manufacturing process, not just for its tensile strength.
Do Not Treat the Forged Condition as the Final Mechanical Condition
For heat-treatable 2xxx alloys, forging establishes the shape and deformation structure, but the required mechanical properties are normally achieved through a specified solution-treatment and aging condition.
T4 and T6 are common examples, but the correct temper depends on the alloy, uber forma, et applicationem.
T4 generally provides a useful combination of strength and ductility, while higher-strength aged conditions can provide greater strength.
For a load-bearing component, the drawing should clearly define the required alloy and temper.
Never assume that a forged part can be used directly simply because the forging itself looks sound.
Control the Starting Material
I always tell young engineers: do not try to fix poor billet quality with a good die.
The starting stock must meet the specified alloy chemistry and applicable material standard.
Chemistry verification and traceability are especially important for 2xxx alloys because composition affects strength, ROSIO, calor, and forging response.
Rather than relying on the phrase “primary aluminum” alone, verify the material specification, chemical analysis, batch identification, and traceability documentation.
A stable forging process starts with stable material.
Choose a Forging Supplier for Process Capability, Not Just Press Tonnage or Price
2xxx alloys can be unforgiving. Higher deformation resistance, temperature sensitivity, and tighter process control requirements mean that an inexperienced forging shop can quickly run into cracking, underfill, tenens, nimia mico, seu dimensiva instabilitas.
When evaluating a supplier, I would look beyond the quoted price and ask:
Can they design the preform? Can they control billet temperature? Do they understand 2xxx die filling?
Can they heat treat and inspect the forging properly? Can they machine the finished component?
Press capacity matters, but a 2,000-tonne press does not automatically make a good 2xxx forging.
The real capability is in the combination of material control, die engineering, forging experience, calor, Cnc machining, et inspectionem.
Faq
Can 2xxx aluminum be forged?
Sic. 2xxx is hot forged within a controlled temperature window, typically around 430–460°C initial forging temperature, with a final forging temperature not below roughly 350–380°C.
Equipment tonnage must be adequate due to higher deformation resistance.
What is the difference between 2A12 and 2024?
They are close counterparts. 2024 is the international designation; 2A12 (formerly LY12) is the Chinese grade widely used in domestic industry.
Properties are similar, but chemistry tolerances and supplier certifications differ—always verify to the applicable standard.
What forging defects are common in 2xxx?
Cracking and incomplete fill are the main risks, caused by a narrow temperature window and high deformation resistance.
Overheating can cause burning; underheating causes cracking. Folding and laps occur when die design or press tonnage is inadequate.
What temper is used after forging 2xxx?
T4 (solution + natural aging) for ductility and machinability, or T6 (solution + artificial aging) for higher strength.
The choice depends on load path, fatigue requirements, and downstream machining.
Can XuChang DEZE forge 2xxx series alloys?
Sic. We cover 2A12, 2014, and other 2xxx grades using certified primary aluminum ingot.
Our equipment includes 300T–2500T precision forging presses and cold forging machines, supporting hot, cold, and hybrid processes.
Send us your drawing for a free DFM analysis covering feasibility, process route, and cost estimate.

