Ma luna o koʻu 29 makahiki e hoʻolālā a hana ana i nā hoʻoheheʻe ʻana i ka corrosion-resistant alloy no ka desalination wai kai, aila waho & aila, and marine fluid systems,
I’ve seen one consistent costly mistake: engineering teams specify a duplex or super duplex steel grade on a drawing, and assume any foundry can produce a casting that matches the performance of wrought bar stock.
That is never the case. Duplex stainless steels are notoriously sensitive to casting solidification, ʻO ka mālama wela, and impurity control.
Get any one of those variables wrong, and you end up with a part that has the same nominal chemistry on paper — but 50% lower corrosion resistance, brittle fracture behavior, or hidden internal porosity that leaks under pressure.
For reverse osmosis (RO), multi-effect distillation (MED), and thermal desalination plants, custom precision-cast duplex and super duplex components aren’t just a “nice to have.”
They are the critical barrier against premature failure in high-chloride, ikaika nui, erosion-prone process streams.
This article breaks down alloy selection, casting process engineering, application-specific components, nā hana maʻamau maʻamau, and the process controls that separate field-proven castings from catalog parts that fail early.
1. Why Duplex & Super Duplex Steel Castings Define Desalination Reliability
Seawater desalination systems operate under some of the most aggressive service conditions in industrial fluid handling: 30,000–45,000 ppm chloride concentrations, operating pressures up to 80 bar for SWRO systems, high-velocity flow erosion, and cyclic thermal loading.
Standard 316L austenitic stainless steel fails rapidly in these conditions — pitting corrosion initiates at welds and surface defects within 12–24 months, a me ke kaumaha o ke kaumaha (SCC) can rupture pressure-containing components in under 5 mau makahiki.
Nā kila duplex, with a two-phase ferrite-austenite microstructure, deliver roughly twice the yield strength of 316L, dramatically better pitting and crevice corrosion resistance, and superior SCC resistance in chloride environments.
While wrought duplex tubing and bar stock serve simple linear components, desalination’s most critical parts — pump bodies, ʻO nā hale kūʻai kūʻai, spray distributors, tube sheets — are geometrically complex.
Welded fabrications leave vulnerable weld seams that act as corrosion initiation points.
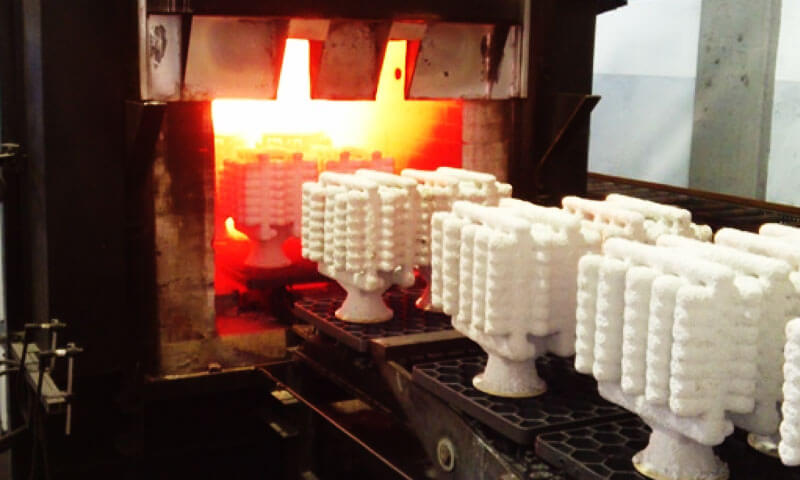
Precision investment casting produces these components as monolithic, seamless parts, with optimized internal flow geometry and uniform material performance across the entire part.
2. Standard Duplex vs. Super Duplex: Nā Kaumaka, Hana & Koho
In desalination applications, the practical difference between standard duplex a Super Duplex is mainly the level of alloying and the resulting resistance to localized corrosion, ka ikaika ikaika, and service margin.
A useful first screening parameter is the ʻO ka heluʻana i keʻano kūlike (Wood), which reflects the contribution of chromium, Mybrideum, and nitrogen to pitting resistance:
Lawe = $ cr + 3.3(%Mo + 0.5%W) + 16%N
As a general engineering classification, conventional duplex grades are commonly in the PREN 30–40 range, while super duplex grades are generally above PREN 40.
PREN is useful for comparing alloys, but it should not be used alone to predict actual desalination performance. Moloka, kūlana pae, keka ao, ka nānāʻana i ka chrlode, and service design all matter.
| Cast Alloy Grade | Typical Alloy Family | Typical PREN Range | Hana Koʻikoʻi | Typical Desalination Applications |
| Cd3mn / ASTM Grade 4A (2205-ʻano) | Standard Duplex | ~ 35 | Good balance of chloride corrosion resistance, ikaika, a me ke kumukuai | SWRO pump casings, nā kino valve, MatifalD, general seawater-contact components |
| CE3MN / ASTM Grade 5A (2507-ʻano) | Super Duplex | ~42+ | Higher resistance to pitting, Kāleʻa Crenice Corrosioni, and chloride SCC than standard duplex | High-pressure SWRO components, seawater intake equipment, pressure-containing housings, severe seawater service |
CD3MWCuN / ASTM Grade 6A |
High-alloy Super Duplex | ~45+ | Enhanced localized-corrosion resistance for particularly aggressive chloride environments | Severe brine service, demanding seawater components, high-corrosion-risk applications |
Selection Guidance
Selection rule of thumb from decades of desalination projects: For standard SWRO plants operating below 70 bar with standard seawater salinity, Cd3mn delivers the best balance of performance and cost.
For high-pressure systems, high-salinity brine, or coastal locations with warm seawater, step up to 2507-grade super duplex.
Reserve premium high-molybdenum grades only for extreme service where 15+ year design life is required.
There is no benefit to over-specifying super duplex where standard duplex will do — material cost increases by 40–60%, and machinability drops noticeably.
3. Why Precision Investment Casting Is the Optimal Process
Many teams ask why we don’t just machine parts from solid duplex bar, or fabricate them from welded plate. The answer comes down to integrity, Hana, a me ka huina kālā.
Integrated, Monolithic Component Geometry
One of the main advantages of Kāhaka kūʻai kūʻai is that complex valve bodies, Nā'āpana pā, MatifalD, and housings can be produced as single cast components rather than assemblies of separately fabricated sections
This eliminates many weld joints and the associated heat-affected zones.
For duplex and super duplex stainless steels, this is particularly valuable because welding requires strict control of heat input, wela waena, filler selection, and subsequent metallurgical condition.
A monolithic casting does not automatically eliminate corrosion risk—casting defects, poino ili, and incorrect heat treatment can still cause problems—but reducing unnecessary welded joints can simplify the corrosion and integrity strategy.
Near-net-shape flow geometry
Investment casting replicates smooth, contoured internal flow paths directly to near-net shape.
Sharp machined steps and weld bead turbulence are eliminated, reducing flow-accelerated erosion by 30–40% compared to machined or fabricated flow paths.
Mea kūponoʻole
For complex pump and valve geometries, investment casting reduces material waste by 60–70% compared to machining from solid bar. With high-value duplex alloys, this delivers enormous cost savings.
Dimensional consistency
Precision casting delivers repeatable dimensional accuracy across production runs, ensuring consistent fit-up for seal faces and piping connections.
4. Critical Process Controls for Desalination-Grade Duplex Castings
The difference between a reliable duplex casting and a defective one is often invisible during visual inspection.
For desalination applications, Ke kū'ē neiʻo Corrosionion, Ke hoʻoikaika ikaika, and service life depend on strict control of the entire manufacturing process, from melting and casting to heat treatment, Machimen, and final surface conditioning.

Melt Chemistry and Impurity Control
The performance of duplex stainless steel is highly dependent on its chemical composition.
For desalination-grade castings, charge materials are carefully controlled to maintain stable and predictable alloy chemistry.
The use of revert material is also limited to reduce the risk of contamination and chemistry variation.
Ma mua o ka nininiʻana, each heat is analyzed using optical emission spectrometry (Poina).
The chemical composition is checked against the specified alloy requirements, with particular attention to chromium, Mybrideum, nickel, a me nitrogen, which directly influence corrosion resistance and ferrite-austenite balance.
Impurity elements such as sulfur and phosphorus are also monitored because excessive levels can negatively affect casting quality and corrosion performance.
PREN can be used as an additional reference when evaluating the alloy’s resistance to pitting and crevice corrosion.
Gating and Solidification Engineering
Duplex stainless steel castings require careful control of filling and solidification, especially for thick-walled pump casings, nā kino valve, and other pressure-containing components.
Poor feeding conditions can produce shrinkage porosity and other internal discontinuities that may not be visible on the external surface.
Gating and riser systems are therefore designed according to the component geometry and solidification characteristics.
The main objective is to achieve controlled solidification and provide adequate feeding to heavier sections.
For critical pressure-containing components, internal quality is verified through appropriate non-destructive testing.
X-ray inspection can be applied to first articles and selected production samples to detect internal porosity, shrinkage, and other casting defects before the components proceed to final machining and assembly.
Solution Annealing and Phase Balance Control
Solution annealing is one of the most critical steps in duplex casting production.
Ma hope o ka hoʻoleiʻana, the components are solution heat treated within the specified temperature range and then rapidly cooled, normally by water quenching where required by the grade and procedure.
The purpose of this treatment is to restore a suitable ferrite-austenite balance and eliminate undesirable intermetallic phases that may have formed during casting.
For desalination-grade duplex castings, the target is generally a balanced two-phase microstructure, with the exact acceptance range determined by the material specification and component requirements.
Keka ao, manawa paʻa, and cooling rate must all be tightly controlled.
An unsuitable heat-treatment temperature, insufficient soaking, or excessive cooling delay can result in an unfavorable phase balance or the formation of detrimental phases such as sigma or chi.
These conditions can reduce corrosion resistance and mechanical performance even though the casting may appear completely normal externally.
Metallographic examination is therefore used to verify the microstructure and phase balance of desalination-grade castings.
Heat-treatment records and metallographic results should remain traceable to the corresponding production heat.
Weld Repair Policy
Weld repair of duplex castings must be strictly controlled because welding changes the microstructure of the weld metal and heat-affected zone.
Any repair welding should be performed only according to an approved procedure appropriate for the specific duplex grade and component.
Where post-weld solution heat treatment is required, the repaired casting must undergo the corresponding treatment to restore the required phase balance and corrosion resistance.
The purpose of weld repair is not simply to remove a visible casting defect.
The repaired area must also meet the same functional and metallurgical requirements as the original casting, particularly for pressure-containing and seawater-wetted components.
Machining and Surface Conditioning
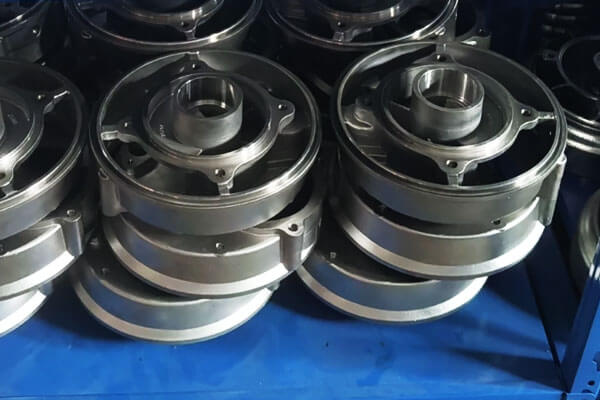
After heat treatment and casting inspection, critical features such as sealing faces, nā lua, e kau ana i na ili, and locating features are precision machined to the specified dimensions and tolerances.
For wetted and flow-related surfaces, surface roughness is also controlled because excessive roughness or machining damage can influence local flow conditions and surface corrosion behavior.
Tool condition, machining parameters, and final surface finish are therefore controlled according to the component’s functional requirements.
Kahi i kuhikuhi ʻia, the final surface is passivated or otherwise conditioned to remove free iron and surface contamination introduced during manufacturing.
This final treatment provides a clean stainless-steel surface and helps preserve the corrosion resistance established through proper alloy selection, controlled casting, ʻO ka mālama wela, a me ke aniani pololei.
5. Corrosion Performance in Desalination Environments
Pitting and crevice corrosion
The desalination environment presents multiple corrosion threats: pitting corrosion from chloride ions, crevice corrosion at gaskets and flanged joints, and stress corrosion cracking under tensile stress in chloride-bearing environments.
Duplex stainless steels offer significant advantages over austenitic grades in all three modes.
Duplex grades have the same or even better corrosion resistance and mechanical strength as their austenitic counterparts.
Compared with cast austenitic steels, they are more resistant to stress corrosion cracking and less susceptible to corrosion fatigue in chloride-containing fluids.
The ranking of corrosion performance in seawater follows a clear hierarchy:
- Super Duplex (Wood > 40) — most resistant to general and localized corrosion attack.
- Standard duplex (PREN 35–40) — suitable for moderate temperature and chloride levels.
- Austenitic 6Mo (Laau ~ 35) — comparable to standard duplex in PREN but lower strength.
- Austenitic 316L (Wood ~ 25) — adequate for ambient seawater but prone to pitting in warm, chlorinated conditions.
Hopena hopena
Temperature is the critical variable that determines whether a given alloy will perform or fail.
The comparative study of wrought SDSS and cast duplex demonstrated that temperature elevation significantly degrades passive film stability.
Both SDSS grades (S32750 and S32760) preserved passivity in synthetic seawater up to 70°C.
The cast alloy DIN/EN 1.4517 lost passivity above 50°C. Impedance values above 5 × 10⁵ Ω·cm² at 25°C decreased with temperature, most significantly for the cast alloy.
Corrosion current densities increased three- to five-fold per 25°C increment.
For desalination applications operating above 50°C—which includes multi-effect distillation and many thermal processes—super duplex castings with proper heat treatment are essential.
Standard duplex may be acceptable at lower temperatures, but the margin for error is small.
Corrosion Fatigue
Desalination pumps operate under dynamic loading conditions. Impellers experience alternating stress as they rotate through the flow field.
Valve components may experience pressure fluctuations. I nā hui chloride, corrosion fatigue becomes a life-limiting mechanism.
Duplex stainless steels are susceptible to chloride-induced SCC and corrosion fatigue, but they clearly offer useful benefits over austenitic grades in terms of cracking resistance.
A ferrite level of approximately 55% is recommended for strength, resistance to corrosion fatigue, and chloride stress corrosion cracking resistance.
6. Failure Analysis: Lessons from the Field
Kālā Kū'ē Manaʻo: Sigma Phase in a Desalination Coupling
The failure of a 6-inch Style D coupling cast from ASTM A820 Grade 2A duplex stainless steel in a desalination plant provides a detailed case study in manufacturing-induced failure.
ʻO keʻano hanaʻole:
Localized corrosion attack leading to cracking and ultimate fracture.
Kumu kumu:
Microstructural analysis confirmed the presence of brittle sigma phase alongside ferrite and austenite in the matrix, which was unusual considering the room-temperature service of the failed coupling.
The sigma phase was introduced during manufacturing due to inappropriate heat treatment and an insufficient cooling rate.
Hoʻoponopono:
Rejuvenation heat treatment at 1200°C for 30 minutes followed by quenching restored the ferrite/austenite microstructure and enhanced corrosion resistance by approximately 30%.
Finite element analysis showed significant residual thermal stresses introduced during quenching, which must be managed through proper cooling practice.
Engineering lesson:
Every duplex casting must have documented solution annealing and quenching records. If the heat treatment is not verifiable, the component should not be accepted for seawater service.
Common Failure Mechanisms and Prevention
| ʻO keʻano hanaʻole | Kumu kumu | Kinohi |
| Sigma phase embrittlement | Slow cooling from annealing; reheating into 600–950°C range | Mandatory water quenching after solution annealing; avoid stress relief in sigma range |
| Pihaʻana | Inadequate PREN; incorrect phase balance; hoʻohaumia ʻili | Specify super duplex for >50lawelawe °C; verify PREN; passivate after machining |
| Kāleʻa Crenice Corrosioni | Weld seams; poor gasket design; ʻO ke komoʻana | Use single-piece castings where possible; proper gasket selection |
Corrosion fatigue |
Potiwale; 'Ōlao'ōmaʻomaʻo; kiʻekiʻe koʻikoʻi koʻikoʻi | Control casting quality; shot peen critical surfaces; design for fatigue |
| ʻO ke kūleʻaʻana o ke kalaʻana | Residual tensile stress; chloride environment | Stress relief at 520°C; avoid high-temperature stress relief |
7. Key Custom Duplex Casting Components in Desalination Systems
Duplex and super duplex castings are particularly valuable in desalination equipment where chloride exposure, Ka paipai, fluid velocity, and complex geometry occur together.
From a foundry engineering perspective, the objective is not simply to select a corrosion-resistant alloy, but to produce a casting with sound metallurgy, geometry hoʻomalu, and enough machining allowance to achieve the final functional dimensions.
High-Pressure SWRO Pump Casings
High-pressure pumps are critical components in seawater reverse osmosis systems.
Their casings must withstand elevated pressure, continuous seawater exposure, hydraulic loading, and potential erosion.
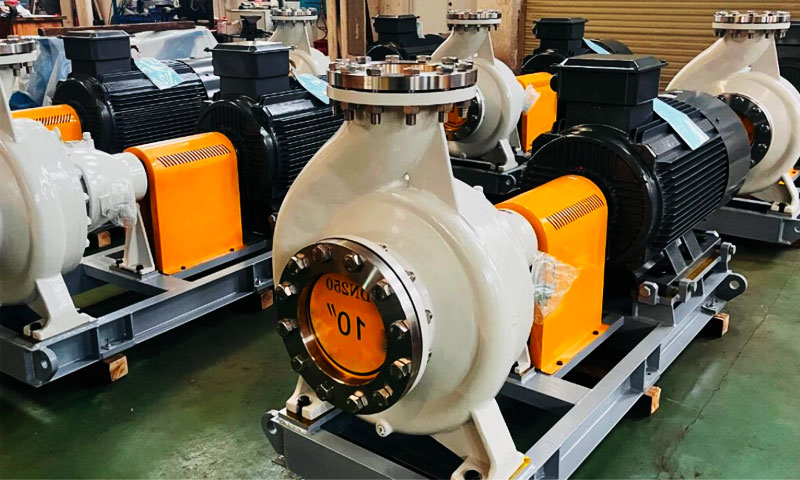
Custom duplex or super duplex cast casings can provide a monolithic pressure-containing structure while allowing complex volute passages, suction and discharge sections, nā iwi iʻa, nā luna kaukaukau, and flange connections to be produced close to their final geometry.
CNC machining then finishes the shaft bore, nā papahele e ana ana, Nā maka o Fladge, and other critical dimensions.
Representative project example: A seawater-service project replaced conventional 316L pump casings after recurring localized corrosion at critical wetted areas.
A duplex cast casing was subsequently selected to provide a higher corrosion-resistance margin while retaining the required pressure and machining capability.
Valve Bodies and Internal Trim Components
Nā Vilves used in desalination plants are exposed to chloride-containing water, nā koina e koi ana, and repeated opening and closing cycles.
The body must maintain pressure integrity while the internal trim must provide reliable sealing and resist local erosion.
Custom duplex cast valve bodies can integrate the main pressure boundary, connection ports, and internal cavities into a single component.
CNC machining then establishes the critical valve seats, nā lua, KauwaiHua, Nā maka o Fladge, a me nā ili hoʻopaʻa.
For more aggressive seawater or brine service, super duplex grades may be selected for components such as seats, plugs, nā papaʻaina, or other flow-exposed trim, depending on the design and corrosion requirements.
Seawater Distributors and Spray Nozzles
Thermal desalination systems and certain brine-handling systems use distributors and spray components to control and distribute fluid flow.
These parts often contain relatively small orifices, nā ʻaoʻao piʻo, and localized high-velocity flow regions.
Investment casting is well suited to these geometries because it can reproduce complex external shapes and internal flow features while minimizing the amount of subsequent machining.
For duplex or super duplex spray components, the casting process should maintain good surface integrity around orifices, flow transitions, and connection areas, since local surface defects can become initiation points for erosion or localized corrosion.
Tube Sheets and Heat-Exchanger Components
Tube sheets are structural components that support large numbers of heat-exchanger tubes and must maintain dimensional stability while exposed to corrosive process media.
The casting route can produce a near-net structural shape, while CNC machining establishes the tube holes, nā helehelena hōʻailona, nā hiʻohiʻona kau ʻana, and other precision interfaces.
Where a component incorporates welded overlays, kukupupuole, or multiple materials, the interfaces become additional areas that require engineering attention.
A homogeneous duplex casting can simplify the material and manufacturing structure when the application is suitable for a cast solution.
Energy Recovery Device Components
Energy recovery devices in SWRO systems operate under high pressure and repeated pressure cycling.
Their internal components therefore require a combination of mechanical strength, Ke kū'ē neiʻo Corrosionion, ʻano kūlike, and good surface condition.
Custom super duplex castings can be considered for selected pressure-containing housings, MatifalD, nā rotors, moe 'ana, and flow-control components, depending on the specific energy-recovery technology.
No kēia mau ʻāpana, dimensional control becomes especially important because small deviations in internal clearances, nā papahele e ana ana, or flow passages can affect operating performance.
8. Duplex 2205 vsa. Super Duplex 2507: How Should Buyers Choose?
For desalination equipment, ʻO ke koho ma waena Duplex 2205 a Super Duplex 2507 should be based on chloride exposure, ʻO ka hanaʻana i keʻano, ʻinoʻino ʻino, Ka paipai, ʻāpana geometry, and required service life—not simply on nominal alloy strength.
For cast components, buyers should also pay attention to the corresponding cast grades rather than specifying only the wrought designations “2205” or “2507.”
Typical cast counterparts include Cd3mn (2205-ʻano) a CE3MN (2507-ʻano).
| Selection Factor | Duplex 2205-Type | Super Duplex 2507-Type |
| Typical cast grade | Cd3mn / ASTM A890/A995 Grade 4A | CE3MN / ASTM A890/A995 Grade 5A |
| Alilolex | Standard duplex stainless steel | Super duplex fuelless |
| Ke kū'ē neiʻo Corrosionion | High resistance to chloride-induced pitting and crevice corrosion | Higher resistance, particularly in more aggressive chloride environments |
| Typical PREN level | Aneane 35 as a general reference | Maki 42+ as a general reference |
| Ka ikaika mīkini | High | Kiʻekiʻe loa |
| Kū'ē i ka chloride SCC | Excellent compared with conventional austenitic stainless steels | Kūpono, with greater corrosion margin in severe service |
| Lawelawe lawelawe | Suitable for many seawater, SWRO, and general desalination components | Preferred where chloride exposure, keka ao, kūlike, or flow conditions are more severe |
| High-chloride brine | Suitable when operating conditions are controlled | Better suited to highly concentrated brine and severe chloride exposure |
| ʻIke wela | Requires proper control to avoid detrimental phase precipitation | More sensitive to thermal exposure and therefore requires particularly strict heat-treatment control |
Nā noi maʻamau |
Nā kāpili pump, nā kino valve, MatifalD, distributors, structural pressure-containing castings | ʻO nā ʻāpana pāpaʻi kiʻekiʻe, severe-service valve bodies, critical wetted components, aggressive brine systems |
| Manufacturing difficulty | Relatively easier to cast, mālama i ka wela, and machine | More demanding because of higher alloy content and tighter metallurgical control |
| Material and processing cost | Haʻahaʻa haʻahaʻa | ʻOi aku ka kiʻekiʻe |
| Buyer priority | ʻO ke kū'ē kū'ē, ikaika, hana ailihua, a me ke kumukuai | Maximum corrosion margin and long-term reliability under severe conditions |
| Recommended selection basis | Moderate-to-severe seawater service where 2205-type performance is sufficient | Severe chloride, concentrated brine, higher temperature, or applications requiring additional corrosion margin |
9. Market Trends and Future Outlook
The global duplex stainless steel market was valued at approximately USD 4.4 biliona i loko 2025 and is projected to reach USD 6.1 biliona ma 2031, achieving a compound annual growth rate of approximately 5.7%.
The desalination segment is a key driver of this growth.
Global demand for fresh water continues to rise, driving expansion of desalination and water treatment plants, particularly in arid regions of the Middle East, North Africa, and Asia-Pacific.
The intense chloride concentrations present in desalination processes make duplex and super duplex stainless steels the material of choice for critical components.
In the United Arab Emirates alone, demand for duplex stainless steel is projected to grow at a CAGR exceeding 7% ma luna o nā makahikiʻelima e hiki mai ana, driven primarily by desalination and water treatment applications.
Three technology trends will shape the future of duplex castings for desalination:
- Higher-alloyed super duplex grades with PREN exceeding 45 for the most aggressive high-temperature, high-chloride applications.
- Mea hoʻohuiʻaha of complex duplex components, offering design freedom beyond conventional casting.
- Digital quality assurance — blockchain-based material traceability and digital heat treatment records for lifecycle management.
10. Hopena
Duplex and super duplex precision castings are the unsung backbone of reliable desalination systems.
They deliver the combination of high strength, excellent chloride corrosion resistance, and seamless monolithic construction that no other material and process combination can match for complex pressure and flow components.
But the grade on the drawing is only the starting point. The real performance is built through controlled melting, engineered solidification, precise solution annealing, and rigorous quality verification.
Cut corners on any of those steps, and you get a part that looks right on paper — and fails prematurely in the field.
Ma hope 29 years in this industry, my advice is simple: don’t source desalination duplex castings on price alone.
The few percent you save on the casting will cost you 10x more in premature replacement, manawa hoʻomaha ʻole, and lost production.
Work with a foundry that specializes in duplex alloys, documents every process step, and validates phase balance and integrity on every heat.
As global desalination capacity continues to expand to meet growing water stress, reliable corrosion-resistant components will remain the most critical driver of plant availability and low lifecycle cost.
Foundries that master the nuance of duplex steel casting engineering will remain central to that growth.
FaqS
Why is solution annealing mandatory for duplex castings?
Solution annealing dissolves sigma phase and other secondary phases that form during solidification and slow cooling.
Without it, the casting will have reduced corrosion resistance, haʻahaʻa haʻahaʻa, and increased susceptibility to cracking.
Solution annealing at 1050–1130°C followed by immediate water quenching is essential.
Can duplex castings be welded?
Duplex castings can be welded with qualified procedures, but the ferrite-to-austenite balance in the weld metal and heat-affected zone must be controlled.
Heat input should be limited, interpass temperature maintained below 100°C, and post-weld solution annealing performed if possible. Field welding is strongly discouraged.
How does cast duplex compare to wrought duplex in corrosion performance?
Cast duplex has a coarser microstructure than wrought, with approximately three times larger inter-austenitic spacing.
This reduces passive film stability, particularly at elevated temperatures.
Kiola 1.4517 loses passivity above 50°C in synthetic seawater, while wrought S32760 resists up to 70°C. Proper heat treatment minimizes this difference but does not eliminate it.
Which ASTM standard covers duplex stainless steel castings?
ASTM A995/A995M covers austenitic-ferritic (Duplex) stainless steel castings for pressure-containing parts.
The equivalent ASTM A890 covers general duplex castings. Grades include 1B, 2A, 3A, 4A, 5A, and 6A, with 5A and 6A being super duplex grades.