
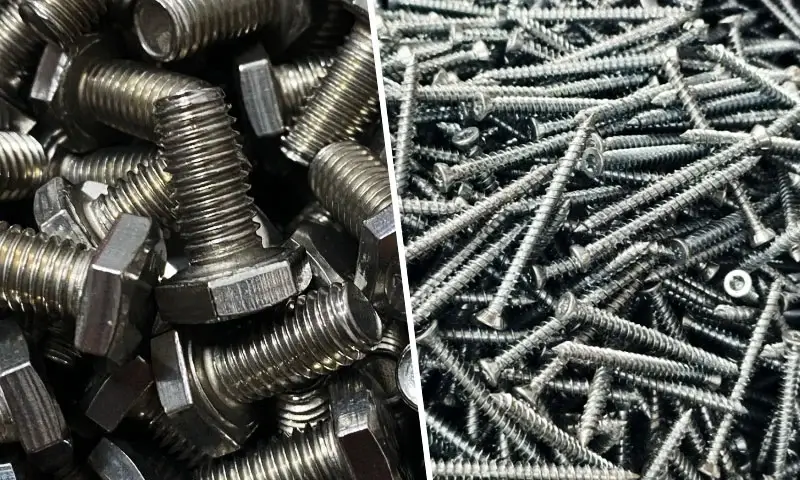
ʻO nā bolts a me nā screws ʻelua o nā mea paʻa mīkini i hoʻohana nui ʻia i ka hana ʻana, kūkulu hoʻi, ʻenekinia kaʻa, ʻO nā mīkini, a me nā huahana o nā lā.
Although they may look similar, they can differ in how they engage with mating components, how clamping force is generated, how they are installed, and which applications they are best suited for.
The terminology also varies among industries, regions, and technical standards.
NOEHUI, selecting a fastener based only on its commercial name can lead to incorrect assumptions about its strength, koi hoʻokomo, or suitability for a particular joint.
This guide explains the differences between bolts and screws from the perspectives of geometry, fastening mechanics, mea waiwai, hana ai.uk, hoʻopiha, a noi aku.
1. Why the Confusion Exists
The terms boltand screware often used interchangeably in everyday language.
A threaded fastener with a hexagonal head may be sold as a bolt in one catalog and described as a screw in another.
The distinction becomes even less obvious when both fasteners have similar heads, thread forms, mea waiwai, a me nā ana.
Three factors contribute to this confusion.
Common usage differs from engineering terminology. In everyday conversation, people may call almost any threaded fastener a screw.
I ka ʻenekinia, Akā naʻe,, the terms can describe different fastening arrangements and installation methods.
Standards do not always use the terms identically. Fastener standards specify dimensions, thread forms, Nā Pīkuhi Propertinies, aiko, and product requirements.
Depending on the applicable standard and product category, a fastener with a particular head and thread configuration may be designated a bolt or a screw.
Appearance alone is not decisive. Hex-head bolts, hex-head screws, socket-head cap screws, and machine screws can share similar external features.
The presence of a pointed tip is also not a universal criterion: many machine screws have flat or blunt ends, while some bolts have specialized end configurations.
For practical selection, it is more useful to examine how the fastener engages the joint, how the load is transferred, and how it is installedthan to rely exclusively on its name.
2. What Is a Bolt?
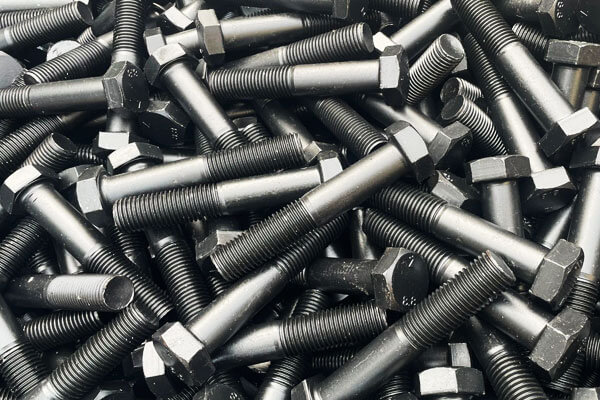
A boltis a threaded fastener commonly designed to pass through aligned holes in two or more components and be secured with a compatible nut.
Tightening the nut, or the bolt head where appropriate, creates tension in the fastener and clamps the components together.
A typical bolt has a head, a shank, and a threaded section. The shank may be partially or fully threaded, depending on the design and application.
Bolts are widely used in structural steelwork, ʻO nā mīkini, nā hui kaʻa, mea paʻi kaomi, and other applications where a joint must withstand tensile loads, shear loads, viguration, or repeated service.
How Bolts Work
In a conventional bolted joint, tightening the fastener stretches the bolt slightly, generating preload, also called clamping force.
This preload presses the joined components together and helps prevent separation or relative movement.
The joint’s performance depends on more than bolt strength. It is influenced by the bolt diameter, thread pitch, papa helu, tightening method, joint stiffness, kūlana pae, and friction beneath the head and nut.
When properly designed, a bolted joint can be disassembled for maintenance without destroying the fastener or the joined components.
Akā naʻe,, repeated use, Kuupuiawi, thread damage, or excessive tightening can reduce reliability.
Common Types of Bolts
| Bolt Type | ʻO ka weheweheʻana | HE KAHUI |
| Hex bolt | Hexagonal head, partially threaded shank, used with a hex nut | Ke kila kila, ʻO nā mīkini, general assembly |
| Heavy hex bolt | Larger head and nut across flats than standard hex | Structural steel connections (A325, A490) |
| Carriage bolt | Round or dome head with a square neck under the head | Wood-to-wood, wood-to-metal; neck prevents rotation |
| Lag bolt | Hex or square head, coarse threads, pointed tip | Wood construction; technically a screw, but commonly called a bolt |
| Plow bolt | Countersunk flat head with a square neck | Plows, nā lako hana; flush surface |
Stove bolt |
Slotted or Phillips round head, machine threads | Light-duty assembly; historically used on stoves |
| Eye bolt | Ring-shaped head | Lifting, tie-down, lele |
| Anchor bolt | Designed to embed in concrete | Structural connections to foundations |
| U-bolt | U-shaped with threaded ends | Pipe clamping, axle mounting |
| Flange bolt | Hex head with integrated flange (washer-like base) | Aitompetitive, ʻO nā mīkini; distributes load |
| Structural bolt | Heavy hex, ikaika-ikaika, specified for structural steel | Nā alahaka, Nā hale, Nā Towers (ASTM A325, A490, F3125) |
3. What Is a Screw?
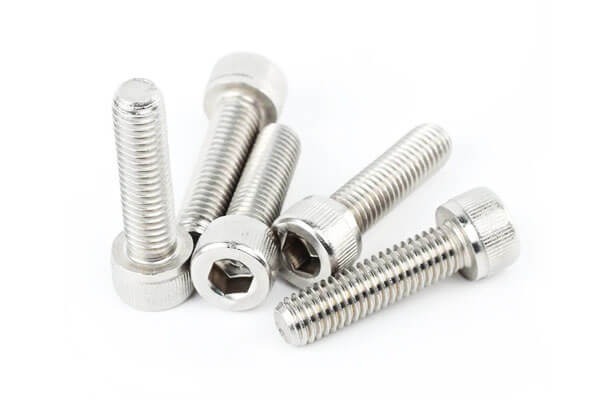
A screwis a threaded fastener designed to engage a mating thread or, in some applications, create its own thread in the material being fastened.
It commonly has a head with a drive feature, such as a slot, Phillips recess, Torx socket, hex socket, or external hexagon.
Unlike a conventional bolt-and-nut arrangement, many screws are installed directly into a tapped hole, a threaded insert, Wood, pale kala, or sheet metal.
Screws are used in products ranging from electronic enclosures and consumer appliances to industrial machinery, precision instruments, nā mea ukana, and building components.
How Screws Work
Screws transfer load through a combination of:
- Ke komoʻana: The threads mate with the material or internal thread, resisting pull-out.
- Clamping force: Similar to bolts, screws create clamping force when tightened, though the mechanics differ because the screw engages the material directly.
- Head bearing: The screw head bears against the surface of the joined part, distributing load.
Screw performance depends on:
- Thread engagement length: Nui, engagement equal to the screw diameter provides adequate strength in steel; softer materials require more.
- Pilot hole size: Critical for self-tapping and thread-forming screws.
- ʻAno kalaiwa: Phillips, slotted, Torx, hex socket, kahua, etc.
- ʻO nā kūpono kūpono: Screw material must be compatible with the joined material to avoid galvanic corrosion or stripping.
Common Types of Screws
| Screw Type | ʻO ka weheweheʻana | HE KAHUI |
| Machine screw | Machine threads, various heads, used with a nut or in a tapped hole | ʻO nā mīkini, nā leka uila, Nā hana hana |
| Cap screw | Socket head (hex socket), machine threads | ʻO nā mīkini, hoao, aitompetitive |
| Self-tapping screw | Forms or cuts its own thread in the material | 'Āpana Mīkini, Nā Plasttics, Wood |
| Self-drilling screw | Drill point; drills and taps in one operation | 'Āpana Mīkini, metal framing |
| Wood screw | Coarse threads, tapered shank, pointed tip | Huakai, nā mea ukana |
Drywall screw |
Fine threads, bugle head, sharp point | Drywall installation |
| Sheet metal screw | Sharp point, fine or coarse threads | Sheet metal assembly |
| Set screw | Headless; used to secure a component on a shaft | Collars, Nā Puke, Nā Knobs |
| Thumb screw | Knurled or winged head for hand tightening | Hoʻoponopono, access panels |
| Shoulder screw | Cylindrical shoulder for pivot or sliding applications | Linkages, hiuntes, pivots |
| Eye screw | Ring-shaped head | Hanging, tie-down |
| Concrete screw | Hākūʻia, high-low threads for concrete | Anchoring to concrete |
| Lag screw | Hex or square head, coarse threads, pointed | Heavy wood connections |
4. Mechanical and Geometric Differences
Bolts and screws can share similar thread forms and head designs, but they often differ in shank geometry, thread engagement, installation methods, and load transfer.
Geometric Differences
Bolts commonly feature a defined unthreaded shank and a partially threaded section, while many screws are fully threaded.
The actual geometry depends on the fastener type, nominal diameter, lōʻihi, a me ke kūlana kūpono.
| Pili | Nā bolts | Nā wilipū |
| Ther Hank | Often includes an unthreaded section to support alignment and transfer shear loads | May be fully or partially threaded, Ma muli o ka hoʻolālā |
| Kila lōʻihi | Frequently partial-threaded in structural and general-purpose applications | Often fully threaded in smaller machine screws; varies by type |
| Head Hoʻolālā | Commonly hex, heavy hex, flange, or carriage heads | Includes socket, Phillips, Torx, slotted, pan, and countersunk heads |
Drive method |
Typically tightened with a wrench or socket | Typically driven with a screwdriver, hex key, Torx bit, or socket |
| Kila ʻano | Commonly metric coarse/fine or Unified threads, such as UNC and UNF | May use standard machine threads, self-tapping threads, or specialized wood-screw threads |
| Lae Hoʻolālā | Usually flat or chamfered | May be flat, pointed, or equipped with a drill point |
| Lunamakaainana kūlā | ASME B18.2.1, ASME B18.2.3, ASTM F3125 | ASME B18.6.3, Iso 7045, Iso 4762 |
Nominal size ranges overlap substantially, so diameter alone cannot reliably distinguish a bolt from a screw.
The applicable product standard and intended joint configuration provide more useful criteria.
Thread Form and Engagement
Bolts and screws may use the same standardized thread forms, including metric coarse, metric fine, Unc, a unf. The key difference is often how the threads engage with the joint.
Bolts typically pass through clearance holes, with the threads engaging a nut or a tapped component.
The unthreaded shank, when present, can help locate the joint and carry transverse loads. Screws may engage pre-tapped holes, nā mea i hoʻopaʻaʻia, or the material itself.
Self-tapping and wood screws use thread geometries designed to form or cut threads in specific substrates.
Coarse threads generally provide faster assembly and better tolerance of minor contamination or damage, while fine threads offer a smaller pitch and finer adjustment of axial position.
Neither is universally stronger or more resistant to vibration; performance depends on fastener dimensions, ikaika waiwai, engagement length, a me ka hoʻolālā hui.
Mechanical Behavior
The primary mechanical difference lies in the joint’s load path and the control of clamping force.
| Hānō | Nā bolts | Nā wilipū |
| Kaumaha transfer | Commonly develop tension in the bolt and compression across the clamped joint | Transfer load through the screw and its engagement with a nut, tapped hole, insert, or substrate |
| Preload Hono | Often established through a specified torque or tensioning method; friction strongly affects the result | Also depends on torque and friction, with greater variability possible when threads engage directly with softer materials |
| MAKAINA WAU ola modes | Tensile fracture, ʻO ka momonaʻole, thread stripping, or joint separation | Screw fracture, drive recess damage, head failure, or stripping of the engaged material |
Hana luhi |
Can be predicted using established fastener and joint-design methods | Depends on fastener geometry, thread engagement, substrate properties, a me ka hoʻouka ʻana |
| Viguration kū kū'ē | May require locking nuts, Nā Kūlana Kūlana-Locking, or other validated retention methods | May require similar retention measures, particularly where the substrate or threaded engagement can loosen or degrade |
5. Bolts vs Screws: Core Differences Explained
The practical differences between bolts and screws become clearer when their fastening arrangements, installation methods, and typical applications are compared directly.
| Kumu Hoʻohālikelike | Nā bolts | Nā wilipū |
| Typical fastening arrangement | Commonly passes through clearance holes and is secured with a nut | Commonly engages a tapped hole, insert, or material directly |
| Mating component | Often a nut, though some bolts engage threaded holes | Often an internally threaded component or the substrate itself |
| Thread configuration | May be partially or fully threaded | May be fully or partially threaded, Ke hilinaʻi nei i ka hoʻolālā |
| Installation tools | Wrench, socket, torque wrench, or specialized tooling | Screwdriver, hex key, socket, or powered driver |
| Clamping force | Commonly generated by tightening the bolt-and-nut assembly | Commonly generated by tightening the screw into its mating thread |
Disassembly |
Usually straightforward if the nut and threads remain accessible and undamaged | Depends on thread engagement, substrate condition, and screw design |
| Typical failure risks | Tensile fracture, Kaluhi, thread stripping, loosening, or joint slip | Drive recess stripping, thread stripping, pull-out, Kaluhi, or loosening |
| Common applications | Structural joints, nā mea hana mīkini, flanges, nā hui kaʻa | Nā pā, electronic products, nā mea ukana, ʻO nā mīkini, and sheet-metal assemblies |
| Design considerations | Bolt strength, nut compatibility, preload, grip length, and joint stiffness | Ke komoʻana, ikaika substrate, drive design, installation torque, and pull-out resistance |
One important qualification is that these are typical practices, not absolute rules. A fastener called a bolt may be installed into a tapped hole, while a screw may be used with a nut.
The applicable standard, product design, and fastening arrangement determine the more precise classification.
Which Provides a Stronger Connection?
Neither bolts nor screws are inherently stronger in every application. Joint strength depends on the fastener’s dimensions, papa helu, thread geometry, engagement length, installation preload, and the strength of the connected materials.
A properly designed high-strength bolt can provide substantial clamping force in a structural joint.
A properly sized socket-head screw can also provide high clamping force in a compact machine assembly.
I kēlā me kēia hihia, the joint may fail before the fastener itself if the threads strip, the substrate deforms, or the connected parts cannot withstand the applied load.
6. Materials and Coatings for Bolts and Screws
The material and surface treatment of a bolt or screw determine its tensile strength, Ke kū'ē neiʻo Corrosionion, ʻano ʻaʻahu, and suitability for specific operating conditions.
Selection should consider mechanical loads, ka hōʻike honua, keka ao, and compatibility with the materials being joined.
Base Materials
The appropriate choice depends on the required strength, Ke kū'ē neiʻo Corrosionion, Ke kaumaha, a me ka puni lawelawe.
| Waiwai | Nā Papa maʻamau |
| Ke kila kalapona haʻahaʻa | SAE Grade 2, ISO property class 4.6 |
| Ke kila kalapona waena | SAE Grade 5, Iso 8.8 |
| Hoʻohuiʻiaʻo Alloy Kōla | SAE Grade 8, Iso 10.9, 12.9 |
| Kila kohu ʻole 304 | A2, 304 |
| Kila kohu ʻole 316 | A4, 316 |
| Ke kila kila ʻole Martensitic | 410 |
| He kila kuhiliʻole paʻakikī ka ua | 17-4 Ph |
| Keleawe a me ke keleawe | C360, C464, keleawe keleawe |
| Titanium | Kumu 2, Kumu 5 (Ti-6al-4v) |
| Apana Apana Aluminum | 2024, 6061, 7075 |
| Nickel alloys | Molol, Actoel |
Ka uhi a me ka lapaʻau ʻili
Coatings improve corrosion resistance, hoʻemi i ka friction, or provide specific surface properties.
| Coating or Treatment | Nā Pōmaikaʻi Nui | Common Applications and Considerations |
| Electrphilabelat zinc | Ka waiwai, moderate corrosion protection | General-purpose fasteners; may require additional passivation or sealing |
| Hot-dip garvalirigigling | Kūlohelohe, durable zinc coating | Outdoor structures and construction; coating thickness depends on the applicable specification and fastener size |
| Zinc-nickel | Enhanced corrosion protection | Automotive and demanding industrial applications |
| Zinc-flake pāpale | Strong corrosion protection with low risk of hydrogen embrittlement during coating application | Automotive and high-strength fasteners |
| Cadmium Wehe | Corrosion protection and useful lubricity | Restricted in many applications because of toxicity; used in certain legacy aerospace specifications |
Phosphate coating |
Provides a base for oil, pehi, or other treatments | Industrial fasteners and components requiring controlled friction |
| ʻeleʻele Oliki | Appearance and limited corrosion protection when oiled | Tooling and indoor applications |
| PTFE-based pāpale | ʻO ka haʻahaʻa haʻahaʻa a me ke kūpaʻa kemika | Applications requiring controlled friction or chemical compatibility |
| Xylan pāpale | Low friction and corrosion protection | Industrial and chemical-service fasteners |
| Dala Wehe | Electrical conductivity and anti-galling properties in suitable applications | Specialized electrical and aerospace assemblies |
| Meaʻole Kukui Kekuhi hoʻolauna | Removes free iron and promotes the protective passive surface | Stainless steel fasteners exposed to corrosive environments |
7. Installation and Tooling
- Access Requirements: Bolts require access to both sides of the joint (one side for the bolt head, the other for the nut).
Screws require access only from the installation side since they mate with internal housing threads. - Torque and Preload: Bolts are routinely tightened using calibrated torque wrenches, hydraulic tensioners, or turn-of-nut methods to achieve precise clamping preload.
Screws are typically driven using standard screwdrivers, Allen keys, or pneumatic torque drivers. - Hiki: Bolted joints can be disassembled and reassembled repeatedly without damaging the parent material.
Screwed joints in soft metals or plastics risk stripping the internal tapped threads over multiple maintenance cycles.
8. Manufacturing Processes of Bolts and Screws
Bolts and screws share many manufacturing processes. Their production routes depend on material, Nā 'Youlelo'Āina, thread design, ikaika pono, TOLECE, paulapua, a me ka hana hana.
Cold Heading and Hot Forging
Cold heading forms a fastener head by plastically deforming wire or rod at or near room temperature.
It is widely used for high-volume production because it offers good material utilization, lawehala, a me ka pono hana.
Hot forging is used when larger dimensions or materials require elevated-temperature forming.
Depending on the design, forging can produce fastener heads and other features that would be difficult to form economically through cold heading.
Thread Rolling and Thread Cutting
Thread rolling forms threads by pressing the fastener blank between dies. It is commonly used for mass-produced bolts and screws and can produce consistent thread geometry without removing material from the thread profile.
Thread cutting removes material with a cutting tool to create the required thread. It is useful for certain specialized designs, ʻO ka hana haʻahaʻa haʻahaʻa haʻahaʻa loa, large fasteners, and applications where the geometry or material makes rolling less suitable.
The choice between rolling and cutting depends on material properties, thread specifications, required production rate, a me ka hoʻolālā ʻāpana.
ʻO ka mālama wela
Heat treatment is used when the specified mechanical properties cannot be achieved through forming alone.
Depending on the steel grade and fastener property class, processes may include quenching and tempering or other controlled thermal treatments.
The purpose is to achieve the required combination of strength, hālulu, and toughness while controlling the risk of excessive brittleness, Kauhai, a me nā hewa'ē aʻe.
Not all fasteners require the same heat treatment. Requirements should follow the applicable material specification and mechanical-property standard.
Surface Finishing and Quality Inspection
Surface treatments may be applied to improve corrosion resistance, hoʻemi i ka friction, or meet appearance requirements.
Depending on the coating, additional controls may be needed to manage dimensional changes, hydrogen-embrittlement risk, or friction variability.
Quality inspection can include checks of:
- Olemela, lōʻihi, head dimensions, and thread geometry
- Mechanical properties and hardness
- Coating thickness and corrosion performance
- Surface defects and material traceability
- Dimensional conformity to the applicable product standard
Standards such as ISO 898-1 for the mechanical properties of specified carbon-steel and alloy-steel bolts, Nā wilipū, a me nā studs, a me iso 3506 for corrosion-resistant stainless steel fasteners, provide relevant frameworks for many applications.
The exact standard depends on the fastener type and specification.
9. Noi: Where Bolts and Screws Are Used
The choice between bolts and screws depends on the assembly design, service loads, installation access, nā koi mālama, and receiving material.
Nā bolts are widely used in structural steel connections, bridge and building assemblies, ʻO Chassis Chassis, nā mea hana mīkini, Nā Flax Flanger, a me nā lako kaumaha.
These applications often benefit from controlled clamping force, accessible nuts, and fasteners designed for defined tensile or shear loads.
Nā wilipū are common in electrical enclosures, mea uila, nā mea ukana, Nā hana hana, sheet-metal products, machine covers, and precision equipment.
They are particularly convenient when the design includes tapped holes or when a fastener must be installed from one side.
Some applications use both. ʻo kahi laʻana, an industrial machine may use high-strength bolts to connect its structural frame, socket-head screws to secure precision components, and self-tapping screws for selected covers or panels.
The correct choice should be based on the requirements of the joint—not simply on which fastener is easier to install.
10. How to Choose Between Bolts and Screws
Selecting the right fastener requires evaluating the entire joint, including the connected materials, kūlana hoʻouka, installation access, a me nā koi mālama.
'Lelo 1: Determine the Joint Configuration
If the components have clearance holes and can accommodate a nut, a bolt-and-nut arrangement may be appropriate.
If the assembly includes tapped holes or threaded inserts, screws may provide a simpler solution.
For thin sheet metal, Nā Plasttics, or wood, specialized self-tapping or thread-forming screws may be more suitable than conventional bolts, provided the substrate can sustain the required loads.
'Lelo 2: Evaluate the Loads
Consider whether the joint will experience tensile loading, pā, viguration, hopena, or cyclic fatigue.
For critical structural or mechanical joints, calculate the required fastener size, ikaika, and preload rather than selecting a fastener by diameter alone.
'Lelo 3: Check Material Compatibility
Select a fastener material that is compatible with both the connected components and the operating environment.
Kuupuiawi, galvanic interaction, keka ao, and chemical exposure can affect long-term reliability.
'Lelo 4: Consider Installation and Maintenance
Evaluate whether both sides of the joint are accessible, whether specialized tooling is required, and how frequently the assembly will need to be disassembled.
Fasteners should also be selected to minimize the risk of drive damage, thread stripping, and loosening.
'Lelo 5: Verify the Specification
Confirm the required diameter, thread pitch, lōʻihi, head style, property class or grade, pāpale, a me ke kūlana kūpono.
For safety-critical applications, follow the engineering drawings, relevant standards, and approved assembly procedures.
11. Common Mistakes When Selecting Fasteners
Several common errors can compromise joint reliability, even when the selected bolt or screw appears suitable.
- Choosing by appearance alone: Similar-looking fasteners may have different thread specifications, Nā Pīkuhi Propertinies, or intended uses.
- Ignoring thread engagement: A screw installed in a weak or insufficiently threaded substrate may pull out before the fastener reaches its rated capacity.
- Using the wrong strength grade: A fastener that is too weak may fail under load, while an unnecessarily high-strength fastener may increase cost or introduce other design considerations.
- Ma luna o ka paʻa: Excessive torque can stretch or fracture the fastener, damage threads, or deform the joined components.
- Ignoring corrosion and galling: The wrong material or surface treatment can cause seizure, accelerated corrosion, or difficult maintenance.
- Mixing incompatible specifications: Thread pitch, olemela, property class, and nut compatibility must be verified rather than assumed.
- Reusing damaged fasteners: Deformed threads, damaged drive recesses, Kuupuiawi, or prior overload may make reuse unsafe or unreliable.
- Neglecting the joint design: Fastener selection alone cannot compensate for inadequate edge distance, weak substrate material, insufficient bearing area, or poor load distribution.
The most reliable fastening solution considers the fastener, mating materials, geometry hui, installation method, and operating environment as one integrated system.
12. Hopena
Bolts and screws perform similar fastening functions, but they are commonly used in different joint configurations.
Bolts typically pass through clearance holes and work with nuts, while screws often engage tapped holes, Pākuʻi, or the material being fastened directly.
These distinctions influence installation, ikaika pipili, mālama, a me ka hoʻolālā hui, although the terminology can vary by standard and application.
Neither type is universally stronger or more reliable. Performance depends on material, Nā 'Youlelo'Āina, thread engagement, preload, geometry hui, a me nā kūlana lawelawe.
Manufacturing processes—including cold heading, Kākau, thread rolling, ʻO ka mālama wela, and surface finishing—also determine whether a fastener meets its specified requirements.
No nā Engineers, mea hanamumu, and purchasing teams, the best approach is to select fasteners according to load requirements, ʻO nā kūpono kūpono, installation access, ʻike ʻino, a me nā kūlana kūpono.
Understanding these factors leads to safer assemblies, more reliable performance, and lower maintenance costs.
FaqS
What is the main difference between a bolt and a screw?
A bolt typically passes through clearance holes and is secured with a nut, while a screw commonly engages a tapped hole, threaded insert, or the receiving material directly.
Akā naʻe,, terminology varies by product standard and application.
Are bolts stronger than screws?
ʻAʻole pono. Strength depends on the material, olemela, thread geometry, mechanical-property grade, a me ka hoʻolālā hui.
A high-strength screw can outperform a lower-grade bolt, while the strength of either joint may be limited by the mating material or thread engagement.
Can a bolt be used without a nut?
ʻAe. Some bolts are designed to engage a tapped hole directly. Whether this arrangement is appropriate depends on the fastener specification, thread engagement, KAUIHOA, a me nā koi noi.
Can a screw be used with a nut?
ʻAe. Some screws, including certain machine screws, can be installed through clearance holes and secured with nuts. The product designation does not always determine the fastening arrangement.
What is the difference between a bolt and a machine screw?
A bolt is commonly associated with a joint secured by a nut, whereas a machine screw generally has machine threads designed to engage a tapped hole or a nut.
Both can have similar head styles and thread forms, so the applicable product standard is important.
What is the difference between a bolt and a stud?
A bolt typically has a head and a threaded shank, while a stud is generally a headless fastener with threads at one or both ends, or along much of its length.
Studs are often used where repeated assembly, alignment, or flange connections are important.

