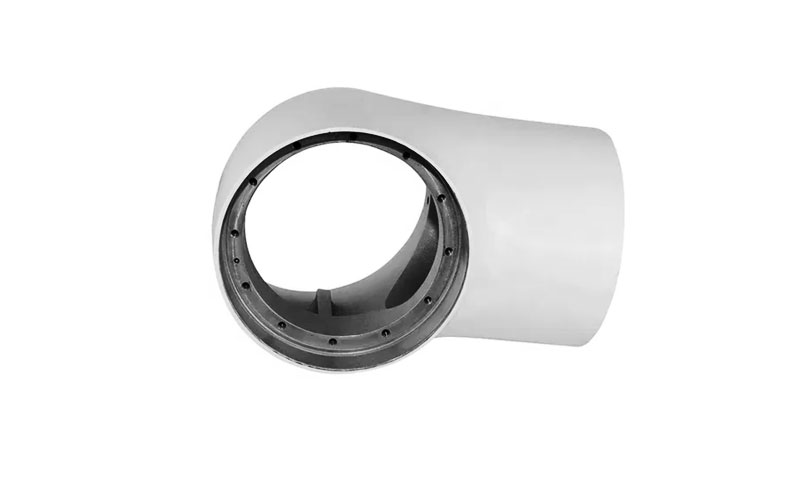
As humanoid robots move from research laboratories into industrial, коммерциялық, and eventually household applications, the demand for lightweight, high-performance structural components is creating new opportunities for the die casting industry.
Magnesium and aluminum alloys are two important material options for these applications. Both offer good castability, relatively low density, and the potential to produce complex, integrated components.
Дегенмен, they do not perform identically, and neither material is suitable for every robotic subsystem.
A common mistake in material selection is to assume that all cast components in a humanoid robot share the same priorities: Салмағы төмен, жоғары қаттылық, жеткілікті күш, and low manufacturing cost.
Іс жүзінде, requirements vary significantly according to component location and function.
A thin-walled forearm housing has different design priorities from a load-bearing hip joint housing or a structural component near the robot’s base.
This guide examines the differences between magnesium and aluminum alloys for robotics castings, explains how requirements vary across humanoid robot subsystems, and discusses how die casting engineers can develop cost-effective manufacturing solutions for these emerging applications.
1. The Segmentation Principle: Different Parts, Different Requirements
The first step in any robot casting project is to segment the robot by function. The table below summarizes the broad pattern I have observed across projects.
| Robot Zone | Primary Requirement | Typical Wall Thickness | Process Preference |
| Forearm, wrist, end effector | Minimum mass, жоғары қаттылық | Thin wall, 1.5– 2,5 мм | Hpdc, thin-wall capable |
| Upper arm, иық | Қаттылық, moderate mass | 2–3 mm with ribs | Hpdc, жартылай қатты |
| Torso, hip | Қаттылық, load transmission | 3-5 мм | Hpdc, жартылай қатты |
| Base, lower body | Тұрақтылық, low center of gravity | Қалың бөлімдер, 5–10 мм | Semi-solid, ауырлық |
| Joint housings | Кию, жылу диссипациясы | 3-6 мм | HPDC with inserts |
| Visible exterior panels | Эстетика, біту | 1.5-3 мм | Hpdc, polished/anodized |
2. Magnesium vs Aluminum Alloys: Fundamental Material Differences
Magnesium and aluminum are both attractive for lightweight die castings, but their physical and mechanical characteristics lead to different design opportunities.
Magnesium alloys offer a lower density, making them particularly attractive for moving components where reducing mass also reduces rotational inertia.
They also provide good vibration-damping characteristics and can be cast into relatively complex thin-walled geometries.
Aluminum alloys generally provide higher elastic modulus, better structural stiffness at the same geometry, and good thermal conductivity.
They also offer a broad range of established casting alloys, Беттік емдеу, and machining solutions.
Key Property Comparison
The following table provides representative engineering ranges. Actual values depend on alloy grade, Кастинг процесі, component thickness, Термиялық өңдеу, and test conditions.
They should not replace the material certificate or component-level design data.
| Мүлік | Магний қорытпалары | Алюминий қорытпалары | Relevance to robotics |
| Тығыздық | Approximately 1.74–1.85 g/cm³ | Approximately 2.65–2.80 g/cm³ | Magnesium can reduce component mass by roughly 30% compared with aluminum at equal volume. |
| Серпімділік модулі | Шамамен 45 Gpa | Approximately 69–72 GPa | Aluminum provides greater stiffness at the same geometry. |
| Specific stiffness (E/ρ) | Approximately 24–26 GPa/(g / cm³) | Approximately 25–27 GPa/(g / cm³) | The stiffness advantage of aluminum is smaller when normalized by density. |
| Жылу өткізгіштік | Approximately 50–100 W/(мом), қорытпаға тәуелді | Approximately 90–220 W/(мом), қорытпаға тәуелді | Aluminum is generally more suitable for heat-spreading structures. |
| Vibration damping | Жалпы жоғарырақ | Жалпы түсуі | Magnesium can help reduce vibration transmission in moving assemblies. |
| Коррозияның мінез-құлқы | Requires careful alloy and surface protection | Generally more established corrosion-protection options | Surface treatment and environmental exposure must be considered. |
Басшылық |
Жұқа қабырғаға тамаша, lightweight components with suitable process control | Кешен үшін тамаша, integrated components; қорытпаға тәуелді | Both can support complex die-cast geometries. |
| Айналымдылық | Жалпы жақсы, but chip and fire-safety controls are essential | Жалпы жақсы, with extensive industrial experience | Both support precision machining of bearing seats and interfaces. |
| Бетті әрлеу | Requires process-specific pretreatment and protection | Broad range of established finishing options | Important for exposed robot housings and exterior panels. |
Маңызды ерекшелік: Magnesium’s lower density does not automatically make a magnesium casting lighter in its final structural application.
Because magnesium has a lower elastic modulus, engineers may need thicker walls, deeper ribs, or additional reinforcement to achieve the required stiffness.
The final weight advantage must therefore be assessed after structural optimization, not from density alone.
3. Жеңіл дизайн: Why Magnesium Is Attractive for Moving Robot Components
In humanoid robots, reducing the weight of moving components is particularly important because their mass directly affects actuator loads and energy consumption.
When a robot extends its arm, the farther the component is from the shoulder joint, the greater its contribution to rotational inertia.
Болғандықтан, the forearm’s weight creates a much greater burden than its mass alone might suggest.
The shoulder and elbow actuators must support not only the arm’s own weight but also the additional forces generated during acceleration, deceleration, and payload handling.
Reducing the mass of the arm structure can therefore lower actuator requirements, improve movement efficiency, or increase the robot’s available payload capacity.
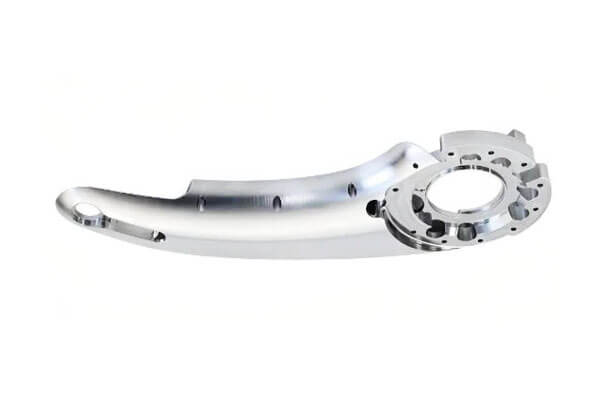
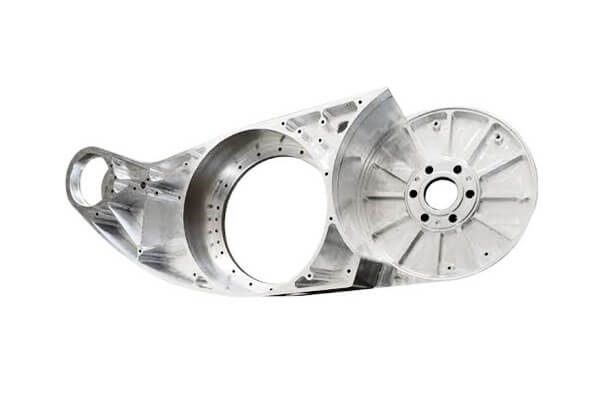
This is where magnesium alloys and thin-wall die castingbecome attractive. Magnesium’s low density helps reduce component mass, while high-pressure die casting (Hpdc) can produce complex housings with thin walls, біріктірілген қабырғалар, and mounting features.
Practical Considerations for Thin-Wall HPDC
Thin-wall design must balance weight reduction with casting feasibility and structural performance:
- Filling limitations:Wall thickness below 1.5 mm can be difficult to fill reliably, particularly when the molten metal must travel a long distance through the die cavity.
- Structural stiffness:Reducing wall thickness also reduces stiffness. Reinforcing ribs and topology optimization are essential to control deformation.
- Жылдам салқындату:Thin sections cool quickly, increasing the risk of cold shuts, толық емес толтыру, and poor surface quality if process parameters are not properly controlled.
- Ejection and handling:Thin-wall castings are more susceptible to deformation during ejection and subsequent handling, requiring carefully designed ejector layouts and support fixtures.
For many robotic arm castings, a wall thickness of approximately 1.5–2.5 mmcan serve as an initial design reference, subject to alloy, геометрия, flow length, and die-casting capability.
A properly engineered rib pattern is equally important.
A flat thin wall may be lightweight but lack sufficient rigidity; a rib-reinforced thin wall can provide a much better balance between mass and structural stiffness.
4. The Base Is Different: Stability Over Lightweighting
Unlike moving components such as robotic arms, castings near the robot’s base prioritize stability over weight reduction.
Appropriate mass at the lower end of the structure helps lower the center of gravity, reduce the risk of tipping, and improve stability during walking, бұру, and other dynamic movements.
Excessive lightweighting in these areas may compromise the robot’s balance and vibration resistance.
, Сорт, base components can use thicker walls and locally reinforced sections where structural loads require them.
Semi-solid rheocastingis a suitable option for such components, particularly when a single casting combines thick bosses, mounting areas, and thin connecting webs.
Key advantages of semi-solid rheocasting for robot base castings include:
- Төмен кеуектілік:Its globular, non-dendritic microstructure and controlled metal flow can help reduce porosity compared with conventional HPDC.
- Better thickness adaptability:It accommodates transitions between thick and thin sections, supporting localized reinforcement without making the entire component unnecessarily heavy.
- Improved mechanical performance:Properly controlled processing can deliver favorable mechanical properties, including elongation and fatigue resistance.
- Reduced oxide entrapment:The less turbulent filling behavior helps limit oxide-film entrainment and improve casting integrity.
This combination of process characteristics is valuable for robot base structures, where designers often need thick load-bearing features alongside thinner sections to control overall mass and maintain structural stability.
5. Heat Dissipation Is a Structural Function
Humanoid robots contain numerous actuators, батареялар, and AI processing units, all of which generate heat during operation.
High-load joints, particularly around the knees and hips, can experience substantial thermal loads.
Some robot designs incorporate heat pipes near the knee joints to provide targeted cooling for high-load actuators.
Болғандықтан, a casting serves more than a structural purpose. Joint housings and supporting components may also function as part of the robot’s thermal management system.
Thermal conductivity therefore becomes an important material-selection criterion alongside strength, қаттылық, және созылу.
This requirement also creates new opportunities for casting alloy development.
Future alloys for robotics applications must balance mechanical performance, Жылу өткізгіштік, and castability rather than focusing exclusively on strength and ductility.
Thermal Conductivity Comparison of Aluminum and Magnesium Alloys
| Қорытпа | Жылу өткізгіштік (М / м /) | Негізгі сипаттамалары |
| A380 (Аль-Си-Ку) | ~96 | Common die-casting alloy |
| A360 (Әл-Си-Мг) | ~113 | Better corrosion resistance |
| A413 (Al-si) | ~121 | Жоғары термиялық өткізгіштік, relatively lower strength |
| Am60 (Мг) | ~62 | Lower conductivity than aluminum alloys |
| Az91 (Мг) | ~51 | Lower conductivity than aluminum alloys |
The comparison shows that these aluminum alloys generally offer higher thermal conductivity than the listed magnesium alloys.
This makes aluminum particularly suitable for joint housings and actuator enclosures that need to transfer heat away from motors and power electronics.
Magnesium remains attractive where reducing moving mass is the primary objective, but its lower thermal conductivity may require additional cooling measures in heat-intensive areas.
For components with demanding heat-dissipation requirements, aluminum is generally the more practical choice; magnesium is more suitable when weight reduction takes priority and the thermal design can accommodate its limitations.
6. Rigidity Matters More Than Ultimate Strength
One important distinction between humanoid robot castings and conventional automotive castings is the emphasis on structural rigidity rather than simply maximizing material strength.
Industry practitioners suggest that, for certain robotics components, once tensile strength reaches an application-specific minimum of approximately 200 МПа, further strength increases may offer less benefit than improving rigidity.
The actual strength requirement depends on the component’s loading conditions, геометрия, and safety factor.
Rigidity is largely determined by structural design. Қабырғаларды нығайту, optimized load paths, generative design, and topology optimization can improve resistance to deformation without relying solely on higher-strength alloys.
A high-strength material in a poorly designed structure can still deflect excessively, while a moderate-strength alloy with an optimized geometry may provide sufficient stiffness and dimensional stability.
Die casting offers considerable design flexibility in this respect. Complex rib networks, variable wall thicknesses, and integrated mounting bosses can be incorporated into a single component, reducing the need for multiple parts and secondary assembly operations.
The key challenge is to ensure that the optimized geometry remains manufacturable and economically viable at the required production volume.
Key Design Considerations
- Design for casting from the outset:Avoid simply converting a machined component into a casting. Қабырғасының қалыңдығы, жобалық бұрыштар, филе, and parting lines should be considered during initial design.
- Use ribs and gussets:Reinforce critical areas to improve stiffness while minimizing additional material.
- Apply topology optimization:Retain material along effective load paths and remove it from areas that contribute little to structural performance.
- Explore generative design:Develop alternative geometries that take advantage of die casting’s ability to produce complex integrated features.
- Validate with FEA:Evaluate deformation, Стресстің таралуы, and load-bearing performance through finite element analysis before finalizing the design and tooling.
For robotics projects, a capable die-casting supplier should contribute to material selection, casting-oriented design, and manufacturability assessment—not simply provide a quotation based on part weight.
7. Impact Resistance and Ductility: Designing for Unexpected Falls
For bipedal humanoid robots, structural rigidity alone is not enough. Unlike stationary equipment, these robots must maintain balance while walking, бұру, and handling objects, which means occasional falls and collisions are unavoidable design considerations.
A robot weighing 80–100 kgcan generate substantial impact loads when it strikes the ground, placing its cast components under loading conditions far beyond normal operation.
This makes elongation and impact toughnessessential material properties. A brittle casting may withstand routine operating loads but crack or fracture under sudden impact.
An elongation of only 0.5%is generally inadequate for components exposed to significant collision risks. The material must provide sufficient ductility to absorb impact energy and resist catastrophic failure.
Conventional die-casting alloys do not automatically meet these requirements.
AlSi9Cu3is widely used for aluminum die-cast components because of its good castability and strength, but its relatively limited elongation and toughness can restrict its use in impact-critical robot structures.
Alloy Considerations for Impact Resistance
| Қорытпа | Typical Elongation | Әсер ету қаттылық | Suitability for Robot Structures |
| AlSi9Cu3 | 1-3% | Байсалды | Limited for impact-critical components |
| A356-T6 | 5-10% | Жақсы | Suitable where heat-treated properties are required |
| A360 | 3-5% | Жақсы | Offers better ductility than conventional AlSi9Cu3 |
| Am60 (Мг) | 6-12% | Жақсы | Good elongation, but lower stiffness |
| Az91 (Мг) | 3-5% | Байсалды | Lower elongation than AM60 |
Ескерту: Elongation and impact performance vary with alloy composition, Кастинг процесі, кеуелік, Термиялық өңдеу, үлгі геометриясы, and test conditions.
The values above are indicative comparisons, not guaranteed component properties.
For impact-critical applications, alloys with higher elongation and toughness are generally preferable.
Термиялық өңдеу, such as T6 for suitable aluminum alloys, can improve mechanical performance.
Дегенмен, it also increases production cost and may cause distortion in thin-wall castings, making dimensional control an important consideration.
Сайып келгенде, humanoid robot castings require a carefully balanced combination of strength, қаттылық, икемділік, әсерге қарсы тұрақтылық, және Қасиеттілік.
Material selection should reflect the component’s actual exposure to collision loads rather than relying solely on conventional die-casting specifications.
8. Magnesium Alloys for Robotics: Артықшылықтары мен шектеулері
Магний қорытпалары are particularly attractive when the main objective is to reduce the mass of moving structures.
Their density is substantially lower than that of aluminum, and their relatively high vibration-damping capacity can be useful in robotic mechanisms.
Дегенмен, magnesium is not an automatic replacement for aluminum. Its lower elastic modulus, Коррозияның мінез-құлқы, surface-treatment requirements, and machining safety considerations must all be addressed.
Key Advantages of Magnesium Alloys
Lower density: Magnesium can reduce the mass of a component by approximately 30% compared with an aluminum casting of the same volume.
This can be valuable for forearms, wrists, ұстағыштар, and other moving structures.
Good vibration damping: Magnesium alloys generally provide better vibration damping than aluminum alloys.
This can help reduce vibration transmission in certain moving assemblies, although the final result also depends on geometry, Буындар, and system-level damping.
Thin-wall casting potential: Suitable magnesium die-casting alloys can produce complex, thin-walled components with integrated ribs, бастықтар, and mounting features.
Жақсы техникалар: Magnesium alloys can be machined efficiently. Дегенмен, өңдеу параметрлері, chip collection, coolant selection, and fire-prevention procedures require specific controls because fine magnesium chips and dust can ignite.
Limitations That Engineers Must Consider
Төменгі қаттылық: Magnesium’s elastic modulus is lower than aluminum’s. A magnesium component may need thicker walls or additional reinforcement to achieve the same deflection limit.
Коррозиядан қорғау: Magnesium alloys can be susceptible to galvanic corrosion when electrically coupled with dissimilar metals in the presence of an electrolyte.
Бекіткіштер, bearing interfaces, жабындар, and drainage design must be considered together.
Бетті әрлеу: Magnesium requires carefully controlled pretreatment and finishing. Not every coating system used for aluminum can be transferred directly to magnesium without process qualification.
Machining safety: Magnesium machining requires suitable chip management, housekeeping, fire-prevention measures, and equipment procedures.
Fine chips and dust present a greater fire hazard than ordinary bulk metal stock.
Material and process qualification: Alloy selection must consider the required casting process, component thickness, Механикалық қасиеттері, коррозияға ұшырау, and applicable safety requirements.
When Magnesium Is Worth Considering
| Component or application | Potential benefit of magnesium | Main design concern |
| Forearm and wrist housings | Reduced moving mass and inertia | Stiffness and impact resistance |
| Lightweight actuator covers | Lower weight and vibration damping | Local mounting strength |
| Robotic grippers | Reduced end-effector mass | Repeated loading and wear at interfaces |
| Moving joint enclosures | Lower rotational inertia | Bearing-seat rigidity and fatigue |
| Lightweight electronic housings | Mass reduction and electromagnetic shielding potential | Thermal management and corrosion protection |
9. Aluminum Alloys for Robotics: Күш, Қаттылық, and Manufacturing Versatility
Алюминий қорытпалары remain highly practical for robotic castings because they combine moderate density with relatively high stiffness, Жақсы жылу өткізгіштік, and a mature manufacturing ecosystem.
They are suitable for a wide range of structural and functional components, including actuator housings, joint structures, motor enclosures, base components, және электронды корпус.
Key Advantages of Aluminum Alloys
Higher elastic modulus: Aluminum alloys have an elastic modulus of approximately 69–72 GPa, compared with roughly 45 GPa for common magnesium alloys.
This makes aluminum attractive where deformation control is critical.
Жақсы жылу өткізгіштік: Many aluminum casting alloys provide effective heat transfer, which is valuable for motor, battery, and electronics housings.
Established die-casting technology: Aluminum high-pressure die casting is widely used for complex components and supports a broad range of production volumes, tooling configurations, and secondary operations.
Flexible surface finishing: Aluminum castings can undergo powder coating, сурет, түрлендіру жабыны, anodizing where the alloy and casting quality permit, and other finishing processes.
Mature machining and joining options: Aluminum components can be CNC machined to achieve accurate bearing seats, бұрандалы тесіктер, герметикалық беттер, and assembly interfaces.
Limitations of Aluminum Alloys
Aluminum is heavier than magnesium, which can increase the inertia of moving robotic components. This is particularly important for long arms and end-effectors.
Some high-pressure die-cast aluminum alloys also have limited elongation, especially when porosity, оксидті пленкалар, or other casting defects are present.
Their suitability for impact-loaded structures must be verified through material testing and component validation.
Thermal conductivity also varies by alloy. An aluminum alloy selected for strength and castability may not provide the highest possible thermal conductivity.
Common Aluminum Alloy Options
The following are examples of aluminum alloys used in die-casting applications. Their suitability for robotics depends on the component’s mechanical, жылу, and manufacturing requirements.
| Қорытпа | General characteristics | Potential robotics applications |
| AlSi9Cu3 | Жақсы күйі, күш, және өлшемді тұрақтылық; widely used in pressure die casting | Жетек машиналары, Автокөліктер, structural enclosures |
| A380 | Жақсы араласу, pressure tightness potential, and general-purpose die-casting performance | Complex housings, Электрондық қоршаулар, mechanical structures |
| ADC12 | Good castability and production consistency in high-volume die casting | Compact housings, қамтиды, and integrated components |
| AlSi10Mg | Good strength-to-weight potential; properties depend strongly on casting route and heat treatment | Structural components where mechanical performance is important |
| AlSi12 | High silicon content and good castability, әсіресе күрделі геометриялар үшін | Thin-wall housings and intricate cast components |
10. Choosing the Right Casting Process: High-Pressure Die Casting vs Semi-Solid Casting
Material selection and casting-process selection should be developed together.
A suitable alloy can still produce an unsuitable component if the process cannot consistently achieve the required wall thickness, Механикалық қасиеттері, өлшемді дәлдік, or internal quality.
Жоғары қысымды өлім
Жоғары қысымды өлім (Hpdc) is well suited to complex, thin-walled robotic housings and components requiring high production efficiency.
Its main advantages include:
- High production rates and repeatability.
- Complex geometry and integrated structural features.
- Good surface finish compared with many conventional casting processes.
- Thin-wall capability with suitable alloy and die design.
- Reduced machining and assembly through functional integration.
Дегенмен, high injection speeds can introduce gas entrapment and turbulence-related defects. These defects may limit the mechanical performance and heat-treatment options of some components.
For robotics castings, engineers should pay particular attention to vacuum control, gate and runner design, басу, local solidification, and the location of critical machined surfaces.
Semi-Solid Die Casting: An Option for Components with Different Wall Thicknesses
Semi-solid casting processes, including rheocasting, use metal slurry containing a controlled solid fraction rather than fully liquid metal.
The material flows into the die under pressure while maintaining a semi-solid microstructure.
This process can be attractive for robotic components with both thin and thick sections, especially where improved filling behavior and reduced turbulence are required.
Potential advantages include:
- More controlled metal flow.
- Reduced turbulence and gas entrapment under suitable conditions.
- Improved potential for producing components with varying wall thicknesses.
- Opportunities to obtain better internal quality and mechanical consistency.
- Compatibility with complex geometries requiring both thin walls and locally reinforced sections.
For a robot arm housing, мысалы, the main shell may be designed with relatively thin walls to reduce mass, while actuator mounting points and bearing supports require thicker sections.
Semi-solid casting may offer a useful process route for this combination.
Дегенмен, semi-solid casting is not automatically suitable for every component.
Slurry preparation, solid fraction, температураны бақылау, толтыру, and process repeatability require close control. Its economic advantage must also be evaluated against tooling, жабдық, Цикл уақыты, Өндіріс көлемі.
11. Беттің қабаты және сыртқы түрі
Unlike many automotive castings, which remain concealed within the vehicle structure, a significant number of humanoid robot castings are externally visible.
Their surface quality therefore affects not only corrosion protection but also the overall appearance and perceived quality of the finished robot.
Die-casting suppliers must pay particular attention to as-cast quality, Бетті дайындау, and finishing consistency.
Visible defects such as flow marks, суық жабдықтар, бетінің кеуектілігі, and uneven textures can make a component unacceptable even when it meets its mechanical requirements.
Дизайнға байланысты, Трастинг, Анодтық, Ұнтақты жабын, or polishing may be necessary to achieve the required appearance.
Дегенмен, the corrosion requirements for many indoor robots differ from those of automotive components exposed to road salt, дымқыл, and changing outdoor conditions.
Robots operating in factories, Қоймалар, and homes may place greater emphasis on appearance, surface cleanliness, and wear resistance than on extreme salt-spray performance.
The actual protection requirements should still reflect the robot’s operating environment.
Surface Finishing Options for Robot Castings
- As-cast surface: Requires consistent quality, with no unacceptable flow marks, суық жабдықтар, or visible porosity in appearance-critical areas.
- Трастинг: Creates a more uniform matte texture and removes surface contaminants and loose residues.
- Анодтық: Provides aluminum castings with a durable oxide layer and, depending on the alloy and process, a range of color options. Magnesium requires specialized surface-treatment processes.
- Ұнтақты жабын: Offers a broad choice of colors, біркелкі қамту, and good surface durability.
- Жылтырату: Improves smoothness and visual quality for exposed components with premium appearance requirements.
Connection design also deserves attention. Unlike many automotive structures that use extensive adhesive bonding, humanoid robot assemblies commonly rely on bolts, Жетекеткіштер, and mechanical interfaces.
Casting features such as flanges, бастықтар, and mating surfaces must therefore provide adequate bearing areas, жіптің қосылуы, and dimensional accuracy to ensure reliable assembly.
Сайып келгенде, surface finishing and connection design should be considered during the casting design stage, rather than treated as secondary operations after production.
12. Why the Best Robotics Casting Solution Starts with the Subsystem
The development of humanoid robots is creating a new opportunity for die casting manufacturers, but it also changes how suppliers need to approach component development.
Traditional casting projects often begin with a drawing, an alloy specification, and a target price. Robotics projects require a broader engineering discussion.
The casting supplier needs to understand where the component is installed, what loads it carries, how it moves, how it connects to other components, and whether it must transfer heat or withstand accidental impacts.
Мысалы, a forearm housing may prioritize low mass and reduced rotational inertia. A knee-joint housing may need greater stiffness, Шаршауға төзімділік, және әсерге төзімділік.
A motor enclosure may require effective heat transfer, while a lower-body structural component may benefit more from rigidity and controlled mass distribution.
A capable die casting manufacturer should therefore provide more than a standard alloy and a production quotation.
The manufacturing solution should consider:
- Material selection based on the component’s actual operating conditions.
- Structural design optimization for stiffness, күш, және салмақ.
- Alloy and casting-process compatibility.
- Дизайн, салу, күшейту, және ақаулардың алдын алу.
- CNC machining of precision interfaces.
- Surface finishing and corrosion protection.
- Шамдық, механикалық, and internal-quality inspection.
-Та Осы, the development of custom cast components can be approached as an integrated process involving casting feasibility, material evaluation, Құралдар дизайны, CNC өңдеу, және әрлеу.
The objective is to help customers turn complex robotic component designs into manufacturable parts with consistent quality.
13. Қорытынды
Humanoid robot castings are not a single market with a single requirement. They are a collection of subsystems with different—sometimes opposite—needs.
The arm needs to be as light as possible; the base may benefit from added mass; the joint housing needs to dissipate heat; the visible panel needs to look good; the falling robot needs toughness, not just strength.
Aluminum and magnesium both have a place in this landscape, but neither is a universal solution. Aluminum offers better stiffness, Жылу өткізгіштік, және бетті аяқтау.
Magnesium offers lower density and better damping, but at the cost of stiffness, термиялық өнімділік, and processing complexity.
The design space for robot castings is wide open. Robots need lightweighting, high rigidity, Жоғары қаттылық, жылу диссипациясы, өлшемді дәлдік, and appearance quality—but not every part needs all of these at once.
The opportunity is to develop casting solutions tailored to each function. That is a far more interesting challenge than competing on price per kilogram.
ЖҚС
Is magnesium better than aluminum for humanoid robot castings?
Not in every application. Magnesium has a lower density and generally better vibration damping, making it attractive for moving components.
Aluminum offers higher stiffness at the same geometry and generally better thermal conductivity.
The choice depends on the component’s load, deformation limits, thermal requirements, және өндірістік шектеулер.
Why is stiffness important for humanoid robot castings?
Stiffness controls how much a component deforms under load. Excessive deformation can affect bearing alignment, gear engagement, actuator positioning, and movement accuracy.
For precision robotic structures, controlling deflection can be as important as achieving sufficient tensile strength.
Why is aluminum commonly used for robot motor housings?
Aluminum combines relatively low density with higher stiffness than magnesium and generally good thermal conductivity.
These properties make it suitable for motor and actuator housings that must support mechanical loads while helping transfer heat away from internal components.
Is AlSi9Cu3 suitable for humanoid robot castings?
AlSi9Cu3 is a widely used aluminum high-pressure die-casting alloy with good castability and useful mechanical properties.
Дегенмен, its suitability depends on the component’s required stiffness, іуу, impact performance, internal quality, және жұмыс шарттары.
It should not be treated as a universal solution for every robotic structure.